- No. 688, Jinji Road, Xiangzhou, Guangdong, China
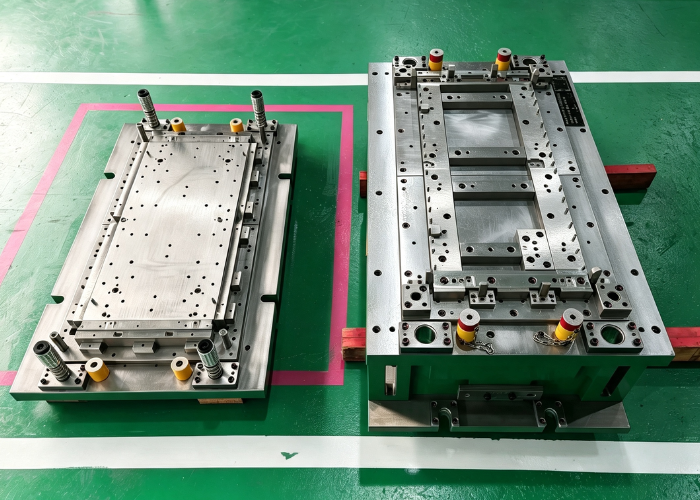
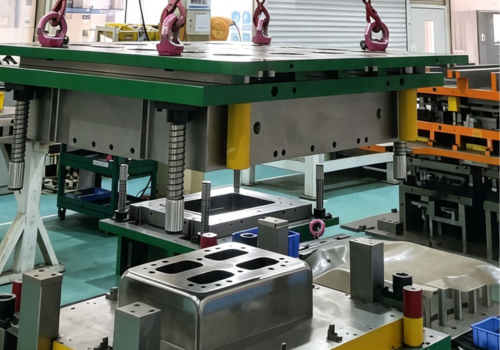
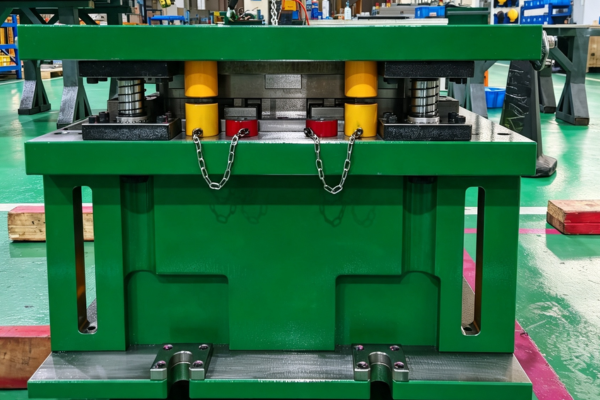
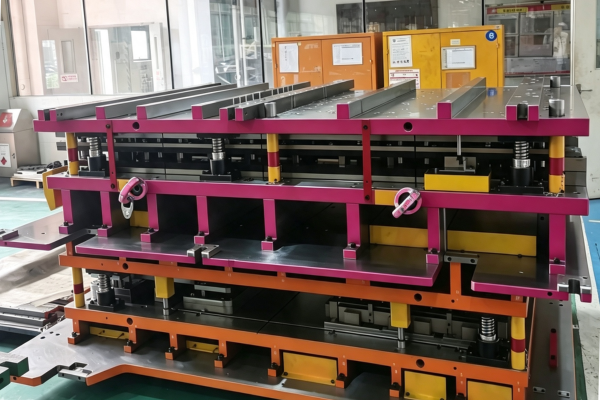
Large deep-drawn sheet metal parts require multiple drawing and restriking operations through several sets of dies and hydraulic press equipment to achieve the final geometry. The key aspects of deep drawing lie in the material’s forming limit, the drawing ratios for multiple operations, as well as the die structure and lubrication factors.
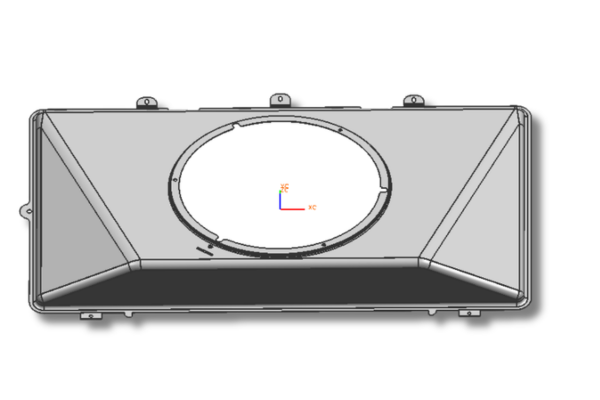
Applied to AC outdoor units, refrigerator side panels, washer drums, and dishwasher panels. Using PCM pre‑coated steel, requiring scratch‑free, orange‑peel‑free, coating‑free surfaces. CAE optimizes material flow and blank holding with nitrogen gas springs, ensuring flatness and gloss consistency for large parts.
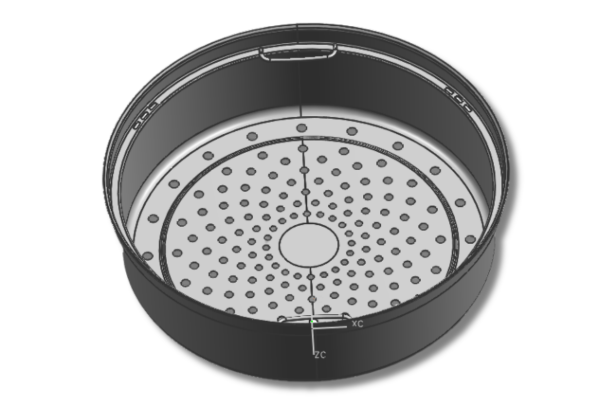
Applied to air fryer baskets, rice cooker steamers, and pressure cooker pots – deep‑drawn parts with high depth, thin walls, prone to cracking/wrinkling. CAE springback analysis and multi‑step drawing + sizing ensure dimensional stability and sealing precision under high depth‑to‑diameter ratios, with food‑grade surface quality.
Applied to electric toothbrush bases, hairdryer housings, and shaver charging cradles – precision micro‑parts. Demanding micron accuracy and long die life. Precision guiding and high‑speed stamping designs control thinning, ensure consistent dimensions and gloss across mass production, meeting consumer‑electronics inspection standards.
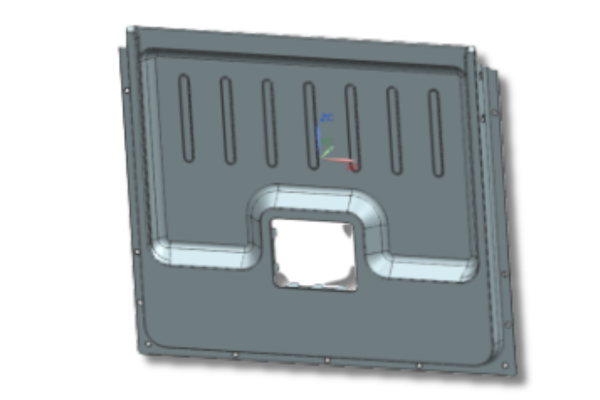
Achieve wrinkle‑free drawing, no invisible cracks, and clear contour lines on the sidewall.
Through CAE analysis, the blank holder force was determined, and the thinning ratio was controlled below 20%. Processes such as drawing, restriking, and side restriking were applied.
• The dimensional tolerance of the protrusions is controlled within ±0.2 mm.
• The product meets the appearance requirements — no wrinkles, no invisible cracks, and clear contour lines on the sidewall.
Gree Daikin offers large deep‑drawing die solutions, using CAE and precision manufacturing to ensure defect‑free forming and stable dimensions for complex stamping parts.
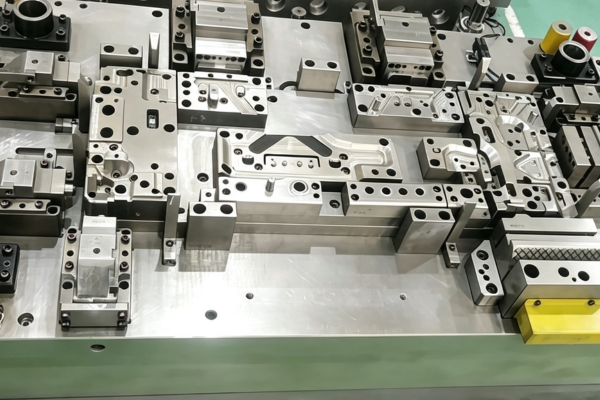
Use angled relief on the female die to reduce side forces; increase male die height for adjustable bulge; reverse‑calculate trim line via CAE and cut after laser tryout; apply profile radius for height differences below 10mm; use slide insert for side tapping/piercing.
The air fryer basket is formed by drawing on a 315T hydraulic press, with strict control to ensure no visible surface defects or burrs. CAE analysis is used in advance to verify the formability of both drawing and sizing operations, thereby optimizing process parameters and ensuring stable dimensional accuracy and satisfactory surface quality
Full‑perimeter undercut triangular ribs without surface defects or seams; 176mm deep draw with no cracking, concavity, or wrinkling; CAE determines M1 drawing and M2 sizing parameters; positioning boss O.D. tolerance ±0.1mm; side undercut uses profile side pusher.
The rice cooker steamer is formed by drawing on a 315T hydraulic press. Strict control over surface quality is required during production to ensure no visible defects or burrs. CAE analysis is conducted in advance to verify the formability of the one‑step drawing and subsequent sizing operations, thereby optimizing die and process parameters to achieve stable dimensional accuracy and satisfactory surface finish.
The part is formed by drawing on a 500‑ton hydraulic press. CAE analysis is conducted to verify formability – one‑step drawing forming ensures a defect‑free surface with no visible imperfections or burrs.
For complex‑surface cavities, angled relief is provided on the female die to reduce lateral forces. The trim line is reverse‑calculated through CAE analysis, followed by laser tryout validation before final trimming die manufacturing.
Tell us your needs, and we will engineer a customized precision die for you. – we’ll get back to you within 24 hours. Your information is secure and will only be used for project consultation.